For sawmills & forestry
Kiln heat and electricity from your offcuts, bark and sawdust
Combined heat and power sized to your mill, running on your own offcuts, bark and sawdust. Start with a free residue and drying-cost assessment.
Already burning residue for heat
Already drying with a wood boiler
If you already burn offcuts and bark to dry your lumber, you have solved the heat. The next step is power. A small combined-heat-and-power (CHP) unit takes the same residue stream and adds self-generated electricity and resilience on top of the heat you already recover — deepening a Scope 1 reduction you have already begun, and lowering both your power cost and your exposure to an outage.
Starting from a disposal cost
Still drying with oil — or air-drying
If you still dry with kerosene or heavy oil, or air-dry, your sawdust, bark, and offcuts are most likely a disposal cost today — hauled away as commercial waste at your own expense. The same daily residue can cover both your drying heat and on-site power at once, ending the disposal cost and displacing the oil bill. This is the clean starting case: residue becomes heat, power, and revenue.
Your residue, in your own terms
A typical unit consumes about 1.6 tonnes of bone-dry fuel a day. In the terms a mill actually measures, that is roughly one skip of chips and sawdust a day — comfortably inside a small mill's own stream, and only a fraction of a mid-sized mill's. We size the unit to your throughput.
What one block means for a mill
The unit behind every figure
One block, on your land
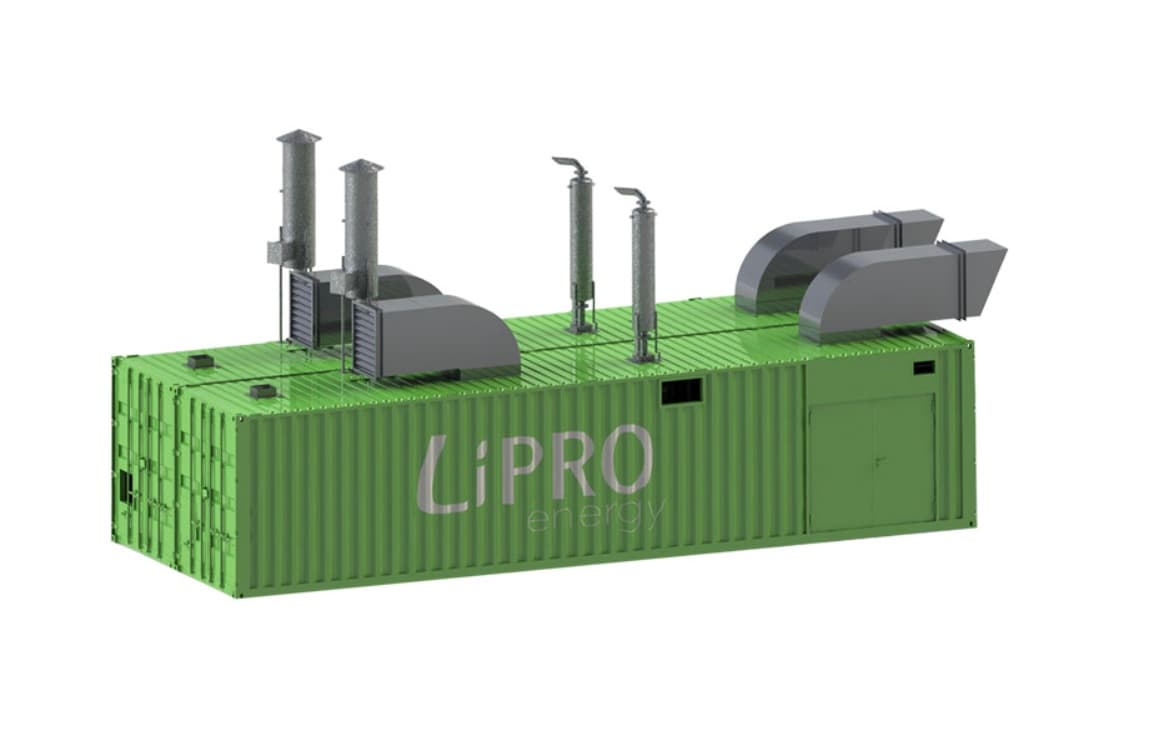
Three LiPRO HKW300 units run in cascade, one CFD dryer, and one moving-floor fuel bay.
Reference design — design figures from the manufacturer specification and our published model, not measurements from an operating plant. No project is sited or in progress. This three-unit reference block is a distinct configuration from the ten-unit data-center block.
Roughly 10,000 m³/yr of log throughput feeds a block on its own — at a 45% sugi residue yield and 0.80 t/m³ green-wood density. Below that, your mill hosts the block and anchors the supply, and we aggregate the rest from neighbouring mills and thinnings — your mill anchors it, it does not have to fill it.
Two options: own the block, or host it. Both run on the same residue and the same block above.
You own it
You finance the block, with forestry facility grants of up to half the cost where a program applies, and we develop and operate it for you. You keep the FIT/FIP entitlement and the savings. Power from your own offcuts falls under METI's general-wood FIT category (¥24/kWh below 10,000 kW), not the ¥40 thinnings category. Large mills such as 銘建工業 and 中国木材 already generate power from their own residue.
Source: MAFF, FY2026 biomass support programs; METI, FIT/FIP tariff table; Meiken Kogyo, biomass power; Chugoku Mokuzai, company profile
You host it
A project company builds, owns and runs the block on your land, buys your residue as fuel, and sells you heat and power below your oil and grid cost. You sign a supply-and-offtake contract instead of taking a loan. Financing is arranged project by project.
Worked examples — we compute your number in the assessment
These are worked examples on stated assumptions, never guarantees. In a free assessment we compute them from your own throughput, kilns, and oil bill.
Heat that fits your kiln schedule
The high-temperature configuration delivers about 100 °C hot water, which covers the 60–90 °C schedules typical of sugi and hinoki structural kiln drying. We are plain about the limit: higher-temperature setting and sterilization stages need a supplementary heat source. We size the system around your actual drying schedule.
Residue is a cost today — it does not have to be
Most mills pay to dispose of bark and sawdust as commercial waste, and carry a drying-fuel bill exposed to every oil-price swing. As an industry example — not an Analema project — one Kyushu mill cut its kiln-drying costs by moving from a heavy-oil boiler to one fired on its own bark. A CHP unit goes a step further than heat alone: the same residue displaces drying fuel and generates power. The assessment works from your own numbers.
It deepens the certifications you already carry
If you hold SGEC or FSC certification or sell J-Credits, CHP on your own residue adds to that record. We design the system around your material, your kilns and the grants available to a mill like yours (林野庁 and NEDO woody-biomass programs).
Common questions
Will 100 °C hot water run my kilns?
For standard sugi and hinoki structural drying, yes — hot-water coils drive the 60–90 °C schedules those kilns run. Higher-temperature setting and sterilization stages need a supplementary heat source, and we say so plainly and design around it.
How much residue does a unit need?
A typical unit takes about 1.6 t/day bone-dry — roughly 3.2 t/day of as-received bark and sawdust, about one skip a day. A small mill's own stream covers it; for a larger mill it is a fraction. We size to your throughput.
We already burn residue for kiln heat. What do you add?
Electricity. The same residue you already dry with can feed a small cogeneration unit that adds self-generated power and outage resilience on top of the heat you recover — deepening a Scope 1 reduction you have already started.
Do you help with subsidies?
Yes. We design the project around the 林野庁 and NEDO woody-biomass grant programs relevant to your mill and include them in the assessment.
Who services the unit, and what if it goes down?
Maintenance is carried out by manufacturer-trained technicians under the service agreement we contract with each host. The block is three independent modules: if one is down for service, the other two still carry roughly two-thirds of the heat, and we stage maintenance around your drying calendar. Your existing boiler is kept as backup, so your kiln schedule never depends on a single unit.
It's a long contract with a young company. What if Analema can't continue?
A fair question, and the answer is in the contract. The term, the exit and step-down terms, and who owns the equipment are all stated up front. Under the host (BOO) structure the block belongs to the project company, so removing it falls to that company, not to you. If Analema were unable to continue, the supply-and-offtake contract and the equipment's ownership are covered by assignment provisions written into that contract, so the arrangement can pass to another operator.